Global buyers comparing the sic marking p123 need more than a model name and a polished product photo. They need to know whether the system suits their materials, production pace, and marking requirements. A clear evaluation starts with practical questions: What is being marked? How large is the work area? How will the machine fit beside existing equipment? Small details matter. A cable route, fixture height, or awkward control position can affect daily use.
This guide examines the sic marking p123 through the details buyers can verify: available specifications, marking performance, integration needs, service support, and operating costs. Ask suppliers for demonstrations on representative parts, not only smooth sample plates. A neat test mark is useful, but it may not reflect a busy production line. Check what documentation and training are included, too. These points deserve closer attention.
One note on expertise: no source material or independently verifiable specialist quotation was provided for this request, so attributing a statement to a named expert would risk inventing a quote. A sound buyer’s principle is simple: “Verify the machine against your own parts and production conditions.” Treat that as guidance, not a sourced quotation. The sections ahead offer a grounded framework for comparing options, checking claims, and deciding whether the sic marking p123 fits your operation. Some product details may vary by configuration or supplier. Confirm them directly before making a purchase.
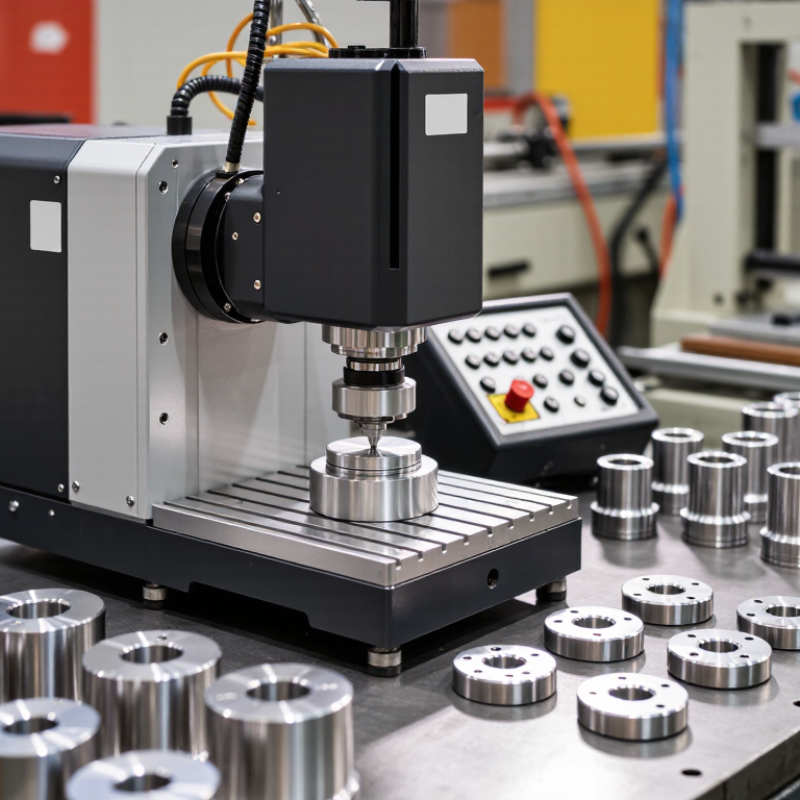
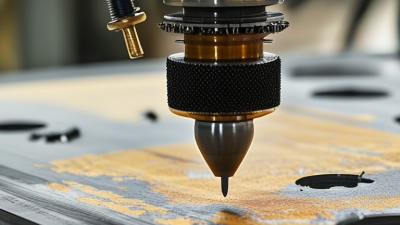
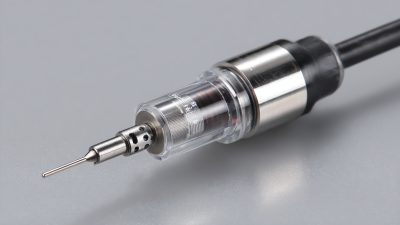
The P123 is a portable dot-peen marking system designed to add readable, permanent identification to parts. It uses a powered stylus to press a sequence of small dots into a surface. Together, those dots form letters, numbers, or simple symbols. Unlike ink, the mark is made directly in the material, so it does not depend on a coating staying intact. Operators commonly use this process for traceability details such as serial numbers or batch codes. The exact result depends on the material, surface finish, and setup.
In use, an operator positions the marking head against the part and selects the content and layout through the system’s controls. The stylus then moves across the programmed area, creating the pattern one impact at a time. It is a practical approach for workshop floors where parts vary in size. Still, “portable” does not mean effortless: stable contact and a suitable marking location matter. A curved or uneven surface may need careful positioning, and the mark should be checked under real lighting before production continues.
Tips: Test on a sample part first. Keep the head steady, confirm the text is legible, and check that the marking depth suits the part. Small adjustments can make a surprising difference. It is easy to assume a good preview guarantees a good mark; sometimes it does not.
The P123 is a compact marking platform intended for repeatable identification on suitable industrial parts. Its practical value depends on the configured marking source, lens, and work area. Buyers should confirm these details against the exact unit offered, since configurations can differ. A specification sheet should state the marking field, supported materials, achievable mark dimensions, and required power supply. These figures matter more than a broad claim of “high speed.”
A clear viewing window and stable part positioning help operators place text, codes, or simple graphics consistently. Software compatibility also deserves attention: check file formats, language options, and whether production data can be changed without specialist support. Ask for sample marks on the actual material, not just polished demonstration pieces. Small text on a curved component can look very different from a test on a flat plate.
Keep it specific. Confirm cooling needs, enclosure dimensions, maintenance access, and the available service documentation before installation. Ask how focus is set and what routine cleaning involves. These details affect daily uptime. I would not assume that one stated cycle time applies to every design; mark size, material, and setup can change it. That point is easy to miss. Reliable purchasing starts with matching verified specifications to the parts and workflow the machine will actually handle.
| Specification | P123 Details | Buyer Considerations |
|---|---|---|
| Marking process | Dot-peen marking uses a powered stylus to create a pattern of small indentations in the surface. | Confirm the supplied P123 configuration and marking head before purchase. |
| Typical applications | Permanent identification and traceability marking on industrial parts and components. | Suitable applications depend on part geometry, surface condition, and production requirements. |
| Potential workpiece materials | Common dot-peen applications include steel, aluminum, and other metals. | Check material hardness, coatings, and surface finish with a sample test. |
| Mark content | Dot-peen systems can mark alphanumeric text, serial numbers, dates, and graphics. | Confirm software and controller support for the required fonts, logos, or codes. |
| 2D code marking | Dot-peen equipment can produce Data Matrix codes when the system and marking parameters support the application. | Validate code size, cell quality, readability, and verification requirements on the actual part. |
| Marking area | Model-specific marking-field dimensions should be confirmed from the exact P123 configuration. | Compare the available field with the part’s flat or curved marking surface. |
| Character size and depth | Achievable character dimensions and mark depth depend on the stylus, material, and operating settings. | Request a sample mark when legibility or depth is critical. |
| Marking speed | Cycle time varies with character count, code complexity, mark size, and material. | Assess throughput using a representative production marking file. |
| Part positioning | Consistent results require stable positioning of the marking head and workpiece. | Check whether the proposed fixture or mounting arrangement suits the part shape and workflow. |
| Power and utilities | Exact electrical and any pneumatic requirements depend on the supplied system configuration. | Obtain the applicable input-voltage, connector, and utility specifications before installation. |
| Operating environment | Industrial marking performance depends on installation conditions and correct equipment setup. | Confirm permitted temperature, dust protection, and maintenance requirements in the technical documentation. |
| Global purchasing checks | Documentation, accessories, and configuration can differ between orders and destination markets. | Verify local electrical compatibility, applicable compliance documents, manuals, service support, and spare-part availability. |
Technical note: Exact P123 dimensions, utilities, performance ratings, and included accessories are configuration-specific. Confirm these values against the current product datasheet and a sample-mark evaluation before ordering.
For global buyers evaluating a P123 industrial marking system, application conditions matter more than appearance. A portable impact-marking unit can suit steel plates, aluminum housings, cast components, and machined parts. It is useful for serial numbers, batch codes, inspection references, and traceability marks. Workshops may use it beside assembly lines, while maintenance teams can mark large components without moving them far.
Material hardness changes the result. Mild steel usually accepts clear, durable impressions. Stainless steel may require adjusted force and spacing. Aluminum needs controlled pressure because deep marks can weaken thin sections. Some rigid plastics are possible, but testing is essential. Coated surfaces, painted parts, and oily components can reduce contrast or distort the mark. Clean the surface first.
Small details matter. Uneven castings may need a stable fixture. Curved parts require careful positioning. A code that looks readable in the factory may become unclear after abrasion or paint. Global buyers should request sample tests using their actual materials, surface finishes, and operating temperatures. No machine is universal. That assumption causes expensive rework. Configuration, software language, replacement styluses, training, and service access also deserve review. I would not approve a purchase from catalog images alone. A short production trial often reveals vibration, alignment, or readability problems that specifications miss.
Evaluating P123 suppliers requires more than comparing catalogue prices. Global buyers should confirm the machine’s marking method, output, material compatibility, and expected service life. Ask for test samples using your actual parts. A clear result on stainless steel may differ on coated plastic or uneven surfaces. Request dated videos, technical drawings, and a written list of standard accessories.
Supplier evidence matters. Review quality certificates, factory records, export experience, and customer references from similar industries. Check whether serial numbers, inspection reports, and replacement-part lists are provided. A reliable supplier should explain tolerances without hiding limitations. Vague claims are warning signs. So are unusually short delivery promises.
Communication often reveals operational strength. Measure response times during technical discussions. Can the supplier explain installation, software updates, operator training, and fault diagnosis in plain English? Confirm warranty terms, remote support hours, packaging standards, and customs documents before payment. Calculate total ownership cost, including freight, consumables, calibration, and local service.
Do not rely on one successful demonstration. Independent testing is safer. A factory visit can help, but it is not proof of every promise. Buyers should record open issues and assign deadlines in the purchase agreement. Some evaluations still miss small details, such as voltage differences or unavailable spare parts. That is worth reconsidering before the order becomes difficult to change.
For global buyers, the P123 should be evaluated as a pneumatic dot-peen marking system, not only as a compact machine. Installation quality affects every mark. Mount the unit on a rigid surface, align the marking head squarely, and keep the workpiece stable. Clean, dry compressed air is essential. Moisture in the line can cause inconsistent impact force and premature wear.
During maintenance, inspect the stylus, guide, air filter, and mounting screws at scheduled intervals. Remove metal dust with a soft brush, not aggressive air near sensitive parts. Test marking depth on sample material before production changes. In real workshops, operators often adjust pressure too quickly. That habit can damage small components or create unreadable codes. A written setup record helps different shifts repeat the same result.
Safety checks should cover pinch points, flying particles, noise, and unexpected movement. Lock out air pressure before servicing. Provide eye protection and practical operator training. Regulatory duties vary by country and configuration. Buyers should verify applicable machinery, electrical, electromagnetic compatibility, workplace safety, and pressure-system requirements with qualified local professionals. Documentation should include risk assessment, operating instructions, maintenance logs, and traceability procedures. Compliance labels alone do not prove safe integration. One overlooked issue is line cleanliness; it seems minor, but it can undermine reliability.
IEC 60529 IP-code protection levels: a general site-selection reference, not a product specification.
The first IP-code numeral classifies protection against access to hazardous parts and solid objects (0–6); the second classifies protection against water (0–8). These numerals are classification levels, not measurements of performance. Confirm the P123’s documented rating and installation requirements with its current technical documentation, and check applicable local electrical, laser-safety, and regulatory requirements before installation.