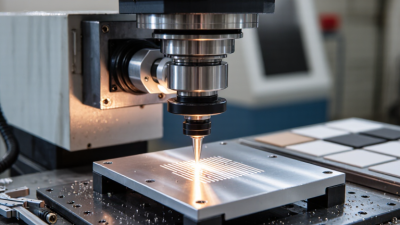
A laser marking machine earns its place on a production line through repeatable results, not impressive specifications alone. For buyers comparing the sic marking c153, the practical questions are clear: Which materials and part sizes must it mark? How consistent must the code remain across shifts? And how easily can operators position each component? Details matter. A clean, legible mark on a flat steel plate does not guarantee the same result on a curved or coated surface.
Market context helps, but it cannot replace application testing. Grand View Research’s laser-marking market analysis estimated the global market at approximately USD 3.3 billion in 2023 and projected continued growth through 2030. That figure signals broad industrial adoption; it does not establish the C153’s performance or suitability for any particular factory. Buyers should request sample marks on their own parts and assess contrast, cycle time, fixture access, and operator workflow. Not every surface behaves alike.
One sourcing limitation deserves candor: I could not verify a published quotation from a named expert specifically about the SIC Marking C153. Inventing one would undermine buyer confidence. Instead, this guide focuses on verifiable checks: confirm the machine configuration with the supplier, review documented specifications, and test representative components before purchase. A short demonstration may reveal issues that a polished brochure misses. The best choice is the one that meets the buyer’s marking requirements consistently, with evidence to support the decision.
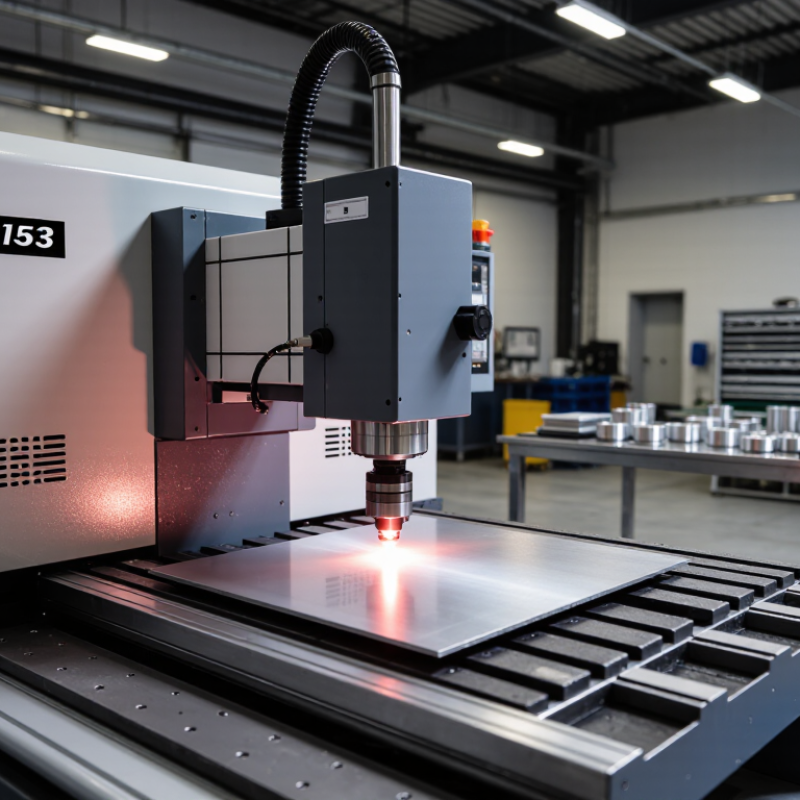
The C153 is an industrial laser marking machine used to place durable text, codes, logos, or other identifiers on components. A focused beam changes the surface of a material, creating a mark without ink or labels. Depending on the machine’s configuration and the workpiece, marking may involve engraving, annealing, or surface discoloration. It is not a one-setting-fits-all tool. Material, finish, and mark depth affect the result.
Its practical role is repeatable identification on parts moving through production or inspection. Operators can adjust marking content and settings for different jobs, but they should confirm legibility and cycle time on actual samples. Grand View Research’s Laser Marking Market report estimated the global market at about USD 3.31 billion in 2023 and projected an 8.0% compound annual growth rate from 2024 to 2030. That broader market trend reflects growing interest in automated, traceable marking; it does not guarantee a particular machine’s performance.
Tips: Test the intended material first. Check code readability under the plant’s lighting, and record settings that produce consistent marks. Ask suppliers to clarify the included laser source, work area, safety enclosure, and support. A polished sample can still hide a weak production process.
The C153 creates a mark by focusing laser energy onto a small, controlled area. Depending on the material and settings, the beam can change surface color, form a contrasting oxide layer, or remove a thin amount of material. The result is more than ink sitting on top. On a stainless-steel part, for example, the mark may appear as a dark, crisp serial code beside a faint heat-affected edge. Focus, speed, power, and surface finish all influence legibility. Small changes matter.
Permanence still needs verification. A strong-looking mark can fade in use if the process only alters a fragile coating. ISO/IEC 29158:2020 provides a direct-part-mark quality method that assesses features such as contrast, modulation, and pattern damage. These checks help teams judge whether codes remain readable, not merely visible on day one. For durability testing, ASTM G154-23 describes controlled fluorescent-UV exposure for nonmetallic materials; it can help evaluate marked polymer surfaces, though it does not replace application-specific testing. Record settings, inspect samples under consistent lighting, then test against the actual cleaning or handling conditions.
A small caveat: “permanent” is not identical across materials. The part, process, and test method must agree.
A C153 laser marking machine can create serial numbers, logos, batch codes, and simple graphics on compatible parts. Suitable materials depend on the installed laser source and surface finish. Common candidates include stainless steel, aluminum, coated metals, and selected plastics. Not every plastic marks cleanly; some may discolor unevenly or produce unwanted fumes.
Typical applications include traceability marks on tools, nameplates, electronic housings, and machined components. A clear mark needs more than adequate power. Focus, scan speed, line spacing, and surface cleanliness all affect contrast and legibility. On a small metal plate, even a slight focus error can soften fine text. Test first. Use sample pieces from the actual production batch when possible.
Marking capabilities range from readable text and one-dimensional codes to detailed two-dimensional codes, depending on software and setup. Deep engraving is not the same as a surface mark, and cycle time can change with mark depth and area. Keep a record of successful settings. Still, a test result on one finish may not transfer perfectly to another; that part is easy to overlook. A brief production trial helps confirm code readability, repeatability, and part fit before routine use.
When comparing the C153 with other laser marking machines, start with the parts you actually need to mark. A clean, dark code on a coated metal housing is not the same task as a shallow mark on stainless steel. Test representative samples, including curved surfaces and slightly oily parts. Look closely at edge sharpness, contrast, and consistency across repeated runs. One sample is not enough.
Check the usable marking area, focus adjustment, fixture clearance, and cycle time with your real production layout. A machine may appear fast on paper but slow down when parts need careful alignment. Ask suppliers to document the tested material, settings, and mark quality; configurations can differ, so confirm the C153 specifications for the exact unit offered. Also compare software usability, operator training, service access, and the availability of replacement components. Small details matter.
Watch the setup.
A practical trial should include a full shift or a representative batch, not just a polished demonstration. Record rejects, repositioning time, and how easily operators repeat the same settings. I would also inspect extraction requirements and workspace fit before purchase. It is easy to overlook these. The best comparison is not the longest specification sheet; it is evidence that the machine produces readable, durable marks at your required pace, with a workflow your team can maintain.
| Comparison factor | C153: what buyers should verify | Fiber laser marker | CO₂ laser marker | UV laser marker |
|---|---|---|---|---|
| Laser source and wavelength | Confirm the supplied laser type and wavelength from the machine nameplate and quotation; model configurations can vary. | Common industrial fiber sources operate near 1,064 nm. | Common CO₂ sources operate near 10.6 μm; other CO₂ wavelengths are also used. | Common UV marking systems operate near 355 nm. |
| Typical material fit | Request sample marks on the exact material, coating, and finish in your production process. | Often selected for metals and some engineered plastics; results depend on material and surface treatment. | Often used for paper, wood, leather, and many other organic materials; compatibility varies by material. | Often considered for plastics, glass, and heat-sensitive products; test the specific formulation and finish. |
| Marking process | Confirm whether the intended process is surface marking, engraving, annealing, or another validated method. | Can mark, engrave, or alter surfaces depending on settings, material, and source configuration. | Can mark or engrave compatible materials; some applications involve cutting as well. | Can produce fine marks on suitable materials; achievable contrast and depth require application testing. |
| Speed and throughput | Ask for a timed sample using your actual mark size, content, material, and required quality. | Often suited to rapid industrial marking, but cycle time depends on the job and system setup. | Throughput varies with material, mark area, power, and required finish. | Throughput varies with mark complexity, material response, and quality requirements. |
| Marking area and focus | Check the lens, usable field size, working distance, focus method, and access to the part. | Field size depends on the selected scanning lens; larger fields can affect spot size and mark quality. | Field size and focus depend on the optical setup and application. | Field size and focus depend on the optical setup and application. |
| Part shape and positioning | Verify fixture requirements, part-height range, rotary-axis options, and marking on curved or uneven surfaces. | A standard 2D scan head is best suited to its specified focal plane; 3D or rotary options may be needed for shaped parts. | Part handling and focus control must suit the geometry and working area. | Part handling and focus control must suit the geometry and working area. |
| Integration and software | Confirm supported file formats, variable-data input, I/O signals, communication interfaces, and line-control requirements in writing. | Integration features vary by controller and machine; verify compatibility with the production line. | Integration features vary by controller and machine; verify compatibility with the production line. | Integration features vary by controller and machine; verify compatibility with the production line. |
| Safety and extraction | Check the laser classification, enclosure, interlocks, applicable local requirements, and extraction needs for the marked material. | Enclosure and protective measures must match the installed laser and applicable safety requirements. | Fumes or particulates may be produced; assess material-specific extraction and fire risks. | Enclosure and extraction requirements depend on the source and material being processed. |
| Ownership and service | Compare warranty terms, service response, spare-parts availability, training, and maintenance requirements. | Compare source and system warranties, service access, and expected consumables for the proposed configuration. | Include extraction, optics, and any application-specific consumables in the maintenance plan. | Compare source warranty, service support, and any application-specific maintenance needs. |
| Best next step | Obtain a written configuration sheet and approve a production-representative sample before purchase. | Shortlist when metal marking or compatible plastic marking is a primary requirement; validate the exact material. | Shortlist when processing compatible organic materials is central to the application. | Shortlist when fine marking or reduced thermal impact is important; confirm results by testing. |
Buyer note: Exact performance depends on the machine configuration, material, mark design, and process settings. Treat the C153 specifications as unconfirmed until they are verified in the supplier’s written documentation and application test.
A laser marking machine should fit the production floor, not just the product brochure. Before purchase, check the available footprint, power supply, extraction needs, and network connections with the installer. Ask who will level the unit, align the marking head, and verify its safety interlocks. Request a trial using your actual part material and surface finish. That matters. A crisp sample on a flat coupon may not match a curved, coated, or oily production part. Record the setup conditions and keep the sample for later comparison.
During operation, assess how easily staff can load jobs, adjust focus, and retrieve approved marking settings. Ask for hands-on training with realistic tasks, such as changing a fixture or correcting a misplaced mark. Check whether operators can identify common faults without guessing. A simple parameter log can help, though it may be neglected during a busy shift. Build it into the normal job record. Also clarify which adjustments require a technician, since frequent trial and error can waste material and slow production.
Ongoing support deserves the same scrutiny as machine performance. Get response-time expectations, remote-support procedures, maintenance intervals, and spare-parts availability in writing. Ask whether service staff can review a sample file or diagnostic report before scheduling a visit. Confirm what training is available when operators change. Support promises sound reassuring, but the useful test is how quickly a real problem gets a clear answer. Keep a record of service contacts, downtime, and recurring faults; it can reveal gaps that a sales demonstration will not.
Suggested evaluation weights for comparing installation, operation, and ongoing support. These are planning weights—not measured performance data—and can be adjusted to fit your application.
Use the weights as a 100-point scorecard. Verify installation requirements and commissioning scope, test marking quality and workflow fit with representative parts, and confirm training, documentation, spare-parts availability, and service response arrangements in writing.