10 Tips for Choosing a SIC Marking E10 Laser Marker

Choosing a SIC Marking E10 laser marker starts with the part, not the brochure. What material needs marking? How large is the marking area? Will the machine mark a flat panel, a curved component, or a part moving along a production line? These details shape the choice of laser configuration, lens, fixture, and software. A crisp sample on a stainless-steel coupon is useful, but it does not prove that the same result will hold across every material or shift.

A practical selection principle is: “Choose the marker around the real part and process, not the ideal sample.” This is an editorial guideline, not a quotation attributed to a named SIC Marking expert. A verified expert name and quotation should be added only when a reliable source is available. That distinction matters. Product advice should be traceable, especially when a purchase affects production quality and uptime.

This guide’s ten tips will help buyers assess marking requirements, machine integration, cycle time, operator access, maintenance, and supplier support. Ask for representative samples. Check whether the marking remains readable after the part’s normal handling and finishing steps. Confirm the available workspace, extraction needs, and installation conditions with qualified personnel. Small details count. A cable route or awkward fixture can slow an otherwise capable system.

The E10 may suit a particular application, but no model is right for every line. Requirements change. Test the actual parts, document the settings, and leave room to question early assumptions. That is a less glamorous step. It is also a useful one.
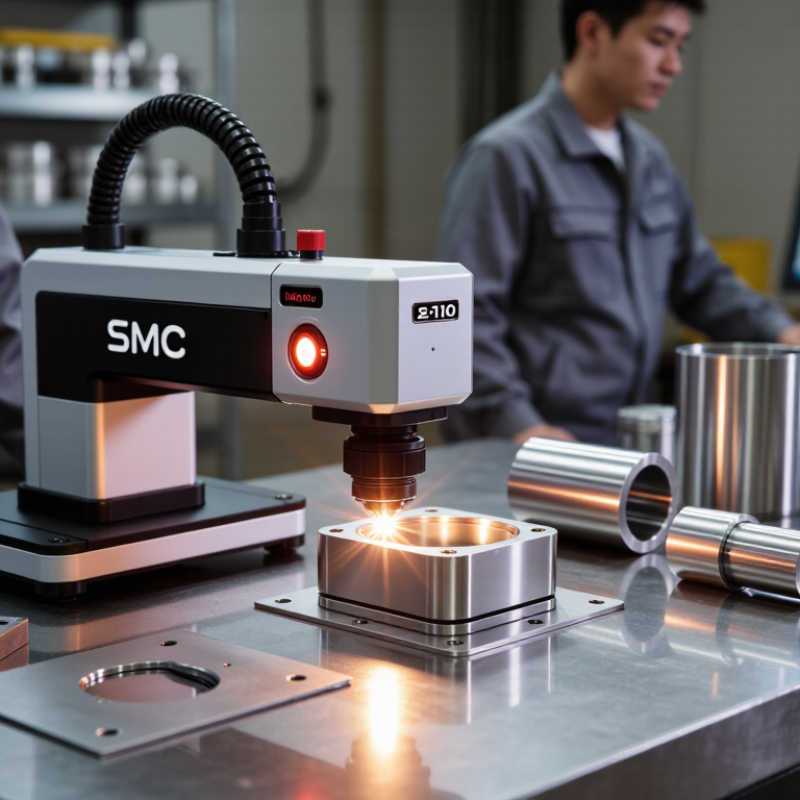
10 Tips for Choosing a SIC Marking E10 Laser Marker

Assess Your Marking Requirements and Production Goals

Before selecting a laser marker, define the job at the workpiece. List each material, surface finish, mark size, and required contrast. A dark anodized part and a polished steel component may need different settings. Test real samples, not just clean, idealized coupons. Include oils, coatings, and normal part variation. Small details matter.

Set production goals in measurable terms: parts per minute, acceptable reject rate, changeover time, and data-recording needs. The International Federation of Robotics reported 4,281,585 industrial robots operating worldwide in 2023, with 541,302 installed that year. This scale of automation makes cycle time and reliable equipment integration practical considerations. Ask suppliers to demonstrate marking speed on your actual parts, within your process limits. A fast scan is not always a fast production cycle.

Tip: Bring a representative batch to testing. Compare legibility after cleaning and handling, then record cycle time and reject rate. Check fixture access, extraction needs, and controller connections before installation. One detail is easy to miss: a mark can look clear on a bench yet become difficult to read under factory lighting. Recheck it on the line.
Check Material Compatibility and Marking Quality

Before selecting a fiber laser marker, test the exact material grade, finish, and coating. Stainless steel may produce a dark annealed mark, while aluminum often needs a different setting for clear contrast. Small changes matter. A polished surface can reflect more energy than a brushed one, and anodized layers may mark unevenly if they vary in thickness. Test real parts, not only sample coupons. Check legibility after cleaning, abrasion, and exposure to heat or oils. A mark that looks sharp on a clean bench can fade in production.

For codes, use a verifier rather than judging contrast by eye. GS1’s General Specifications draw on ISO/IEC 15415, which grades 2D symbols on a 0.0–4.0 scale. That gives teams a measurable quality check, though the required grade depends on the application. Record settings and results for each material batch. Include edge definition, code readability, and mark depth where relevant. I would not assume one preset works across every part; even a small change in coating can undermine repeatability. Try a few power and speed combinations, then inspect the least favorable sample. A slightly slower test now may prevent unreadable marks later.

Compare Laser Power, Field Size, and Cycle Speed

When evaluating an E10 laser marker, compare usable laser power against the materials and marks you actually need. More power can help create a deeper mark or shorten exposure time, but it may also darken or damage a sensitive surface. Test sample parts with the intended finish, not just clean showroom pieces. Check contrast, edge sharpness, and consistency across several runs. Power alone tells you little.

Field size affects both coverage and detail. A larger field may fit multiple components, but small text or codes can lose definition near the edges. It is tempting to choose the largest field. That can be a mistake. Place a sample part at the center and corners, then inspect the smallest feature under normal lighting. Confirm that the working distance suits your fixture and operator access.

Cycle speed should reflect the full production routine, not the laser’s marking time alone. Include part loading, positioning, focus checks, and any required verification. A fast mark is not much help if the operator must realign each part by hand. Run a timed trial with representative parts and your normal batch size. Keep an eye on missed marks and variation between cycles. Small delays add up. The first trial may look excellent, yet a longer run can expose heat buildup or inconsistent positioning; that deserves a second look.

Review Installation, Controls, and Line Integration

Installation starts with the part, not the marker. Check the mounting surface for vibration, then secure the unit where operators can reach it safely. Leave room for cables, ventilation, and routine cleaning. Small spaces become frustrating fast. Measure the working distance with the actual fixture in place; a sample on a bench may sit differently on a moving line. I would also verify that the marked area stays clear of clamps and guards throughout the full cycle.

Controls should feel clear to the person running the shift. Confirm how recipes are selected, how focus is set, and what an error looks like on the screen. Use a test piece with the real surface finish. Dark coatings, curved parts, and reflective metal can behave differently than expected. A quick trial helps, but it may not reveal every production issue. Keep approved settings documented, including any limits operators should not change.

For line integration, map the marker’s start, ready, and fault signals to the controller before installation day. Test the handshake with the conveyor stopped, then at normal speed. Check that the part sensor triggers at the correct position and that a missed mark stops or flags the right station. Timing can be awkward. Leave time for a few imperfect trials; real parts rarely behave as neatly as drawings.

10 Tips for Choosing a Laser Marker: Review Installation, Controls, and Line Integration

Use this checklist to compare laser-marking solutions against your parts, production process, site conditions, and applicable safety requirements.

No. Selection Area What to Review Useful Evidence or Acceptance Check
1 Confirm the marking application Identify the part material, surface finish, mark location, and required content. Marking results can vary with material composition, coatings, and surface condition. Test representative production parts, including normal material and finish variations. Approve samples against the required appearance and readability.
2 Check the installation envelope Measure the available space, access for loading and maintenance, mounting points, cable routes, and the position of nearby equipment. Review a dimensioned layout or on-site measurement. Confirm that the laser head, controller, guarding, and service access fit without obstructing the line.
3 Review mounting and part positioning Determine how parts are located and held during marking. Check working distance, focus adjustment, part orientation, and the repeatability of fixtures or conveyor positioning. Run a positioning trial using the actual fixture or conveyor setup. Verify mark location across the expected range of part tolerances.
4 Verify environmental suitability Compare the installation area's temperature, dust, humidity, vibration, and cleaning conditions with the equipment's documented operating limits. Obtain the manufacturer's environmental specifications and assess whether an enclosure, extraction system, or other site protection is required.
5 Assess utilities and extraction Check electrical supply, grounding, compressed air if required, and the need to remove smoke or process residue from the marking area. Confirm utility requirements in the installation documentation. Include extraction capacity and discharge arrangements in the site review.
6 Evaluate operator controls Review how operators select jobs, edit permitted fields, start or stop a cycle, and respond to alarms. Consider access permissions and language needs. Ask operators to complete typical tasks during a demonstration. Check that job selection and error recovery are clear and documented.
7 Check data and communications List required inputs and outputs, such as job selection, start signals, ready status, fault status, and variable data from a production system. Confirm available communication interfaces and signal definitions in writing. Test data transfer, invalid values, and recovery after a communication interruption.
8 Plan line timing and traceability Compare the marking cycle with the production takt time. Define how each part is associated with its unique code or other variable marking data. Measure cycle time using production-representative content and parts. Validate data matching and record handling with the line's traceability process.
9 Include laser safety in the layout Identify the laser class and required protective measures for the intended installation. Consider guarding, interlocks, access points, warning labels, and local regulations. Request the applicable safety documentation and conduct a site-specific risk assessment with qualified safety personnel before operation.
10 Plan service and acceptance testing Review maintenance tasks, consumables, spare-parts availability, technical support, training, and the process for restoring saved settings or job files. Agree on acceptance criteria for mark quality, cycle time, interface signals, and operator training. Record results from a production-representative trial.

Evaluate Safety, Service, and Total Ownership Costs

A laser marker should fit the real work area, not just the sales drawing. Check the enclosure, access points, and interlocks with the machine installed. Ask how fumes are managed for the materials you actually mark. A sample test can reveal residue, glare, or awkward loading before purchase. Small details matter. Operators also need clear instructions for setup, routine checks, and unexpected stops. A tidy demonstration is useful, but it does not replace a practical safety review.

Service quality affects output long after installation. Ask who handles troubleshooting, how quickly support usually responds, and which parts are kept available. Request a maintenance schedule in writing. Check whether staff training is included, and whether service visits create extra charges. Keep the answer specific. A vague promise of “help when needed” is hard to plan around. I would also ask what happens if a fault appears during a busy production week; the answer may expose gaps in the support plan.

Purchase price is only one part of ownership cost. Include installation, extraction equipment, fixtures, training, maintenance, and expected downtime in the estimate. Compare those costs against your marking volume and planned use. A lower quote can become expensive if setup takes longer or service is distant. Still, estimates are estimates. Build in some room for missed assumptions, then review the figures with the people who will operate and maintain the system.

+1 450 449 9133
Contact us sale@rhythmachine.com